Introduction to High-Capacity Reverse Osmosis Systems
In the realm of industrial water treatment, the demand for high-purity water is ever-increasing. A 100T/H large-scale reverse osmosis (RO) system stands as a cornerstone in modern water treatment plants, delivering exceptional performance and reliability. NPW, a global leader in industrial equipment, presents this advanced solution designed to meet the rigorous needs of food processing, livestock operations, and other industries requiring vast quantities of purified water.
Key Features and Technical Advantages
This 100T/H RO system is engineered with cutting-edge technology to ensure optimal water quality and operational efficiency. The system utilizes high-quality stainless steel construction for all wetted parts, ensuring durability and corrosion resistance. The multi-stage pre-filtration process removes large particles and chlorine, protecting the RO membranes. The heart of the system, the spiral-wound RO membranes, are arranged in a sophisticated configuration to maximize recovery rates and minimize energy consumption.
- High Flow Rate: Capable of producing 100 tons of permeate per hour, suitable for large-scale operations.
- Precision Control: Equipped with PLC automation for real-time monitoring of pressure, flow, and water quality.
- Energy Efficiency: High-efficiency pumps and energy recovery devices reduce power consumption.
- Modular Design: Skid-mounted for easy installation and expansion.
Applications in Food Processing and Livestock Industries
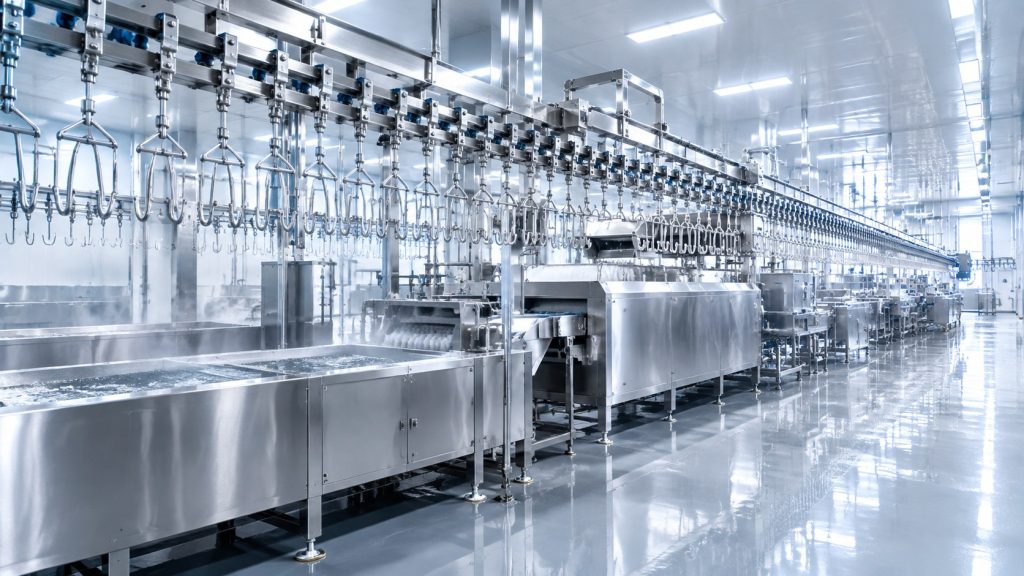
In food processing, water quality is paramount. This RO system provides water that meets stringent hygiene standards, essential for slaughter lines, washing, and ingredient water. For livestock operations, purified water ensures animal health and biosecurity. NPW’s integrated approach ensures that this water treatment solution seamlessly integrates with other processing equipment, creating a cohesive production line.
Quality Assurance and Delivery
At NPW, every 100T/H RO system undergoes rigorous testing before shipment. From membrane integrity checks to full-load performance tests, we guarantee that each unit meets our exacting standards. Our professional packaging ensures safe delivery worldwide, with comprehensive documentation and support for installation and commissioning.
“NPW’s 100T/H RO system has revolutionized our water supply, providing consistent high-purity water for our entire processing plant.” – Satisfied Client
Conclusion
Investing in a 100T/H large-scale reverse osmosis system from NPW means investing in reliability, efficiency, and unparalleled water quality. With our commitment to innovation and customer satisfaction, NPW continues to lead the way in industrial water treatment solutions. Contact us today to learn how this system can transform your operations.
Solutions related to this article
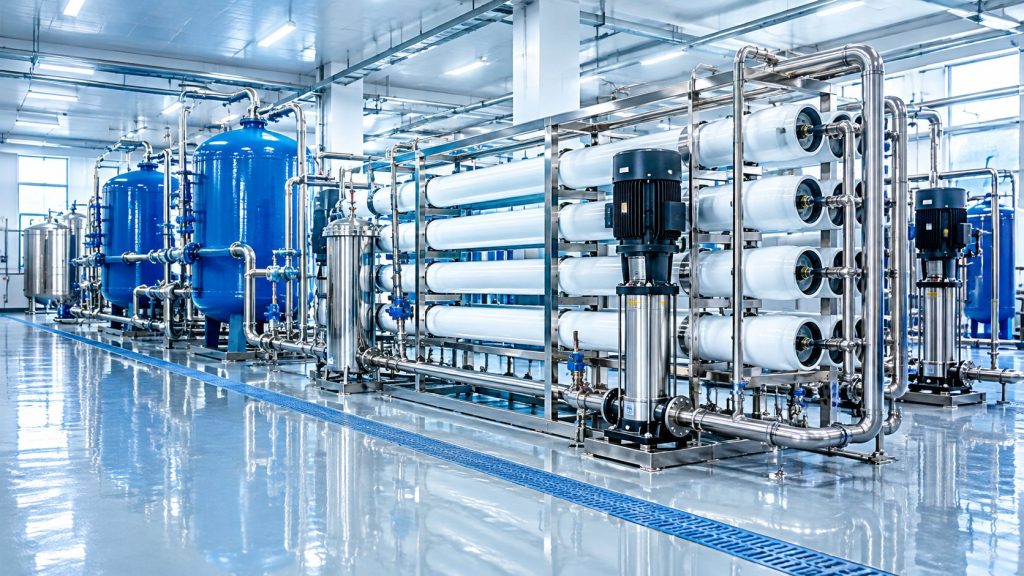 WaterWater Purification Equipment SolutionTreatment and reuse for process water, scalding tanks and plant supply.View solution →
 CleaningFood Industry Cleaning Equipment SolutionsFoam, CIP and washdown systems for food-contact surfaces and drains.View solution →
 PoultryComplete Poultry Slaughter Line SolutionsHanging, scalding, plucking, evisceration and chilling on one continuous line.View solution →