Introduction to 0.5 T/H Reverse Osmosis System
In the food processing industry, water quality is paramount. The 0.5 T/H reverse osmosis (RO) system from NPW is designed to deliver high-purity water for various applications, ensuring product safety and quality. With a capacity of 0.5 tons per hour, this compact yet powerful system is ideal for small to medium-scale food and beverage production facilities.
Key Features and Benefits
- High-Efficiency Filtration: The system utilizes advanced RO membranes to remove up to 99% of dissolved salts, bacteria, and organic matter, producing water that meets stringent food-grade standards.
- Compact Design: The 0.5 T/H capacity is perfect for operations with limited space, without compromising on performance.
- Durable Construction: Built with food-grade stainless steel and corrosion-resistant components, ensuring longevity and hygiene.
- Automated Control: Equipped with PLC control for automatic operation, reducing labor and minimizing human error.
- Low Maintenance: Easy access to filters and membranes simplifies maintenance, reducing downtime.
Applications in Food Processing
This RO system is versatile and can be integrated into various food processing lines:
- Beverage Production: Provides consistent water quality for beverages, ensuring taste and shelf life.
- Ingredient Water: Used in recipes where water quality affects flavor and texture.
- Equipment Cleaning: Supplies pure water for CIP (Clean-In-Place) systems, preventing contamination.
- Boiler Feed: Reduces scale buildup, extending equipment life.
Why Choose NPW’s RO System?
NPW is a trusted name in food processing equipment, known for reliability and innovation. Our 0.5 T/H RO system is engineered for optimal performance, with a focus on energy efficiency and ease of use. Backed by our global service network, you can trust NPW to support your production needs.
“Water purity is not just a requirement; it’s a commitment to quality. NPW’s RO systems help you uphold that commitment effortlessly.”
Conclusion
Investing in a 0.5 T/H reverse osmosis system from NPW is a smart move for food processors looking to enhance water quality, comply with regulations, and improve operational efficiency. Contact us today to learn more about how this system can benefit your facility.
Solutions related to this article
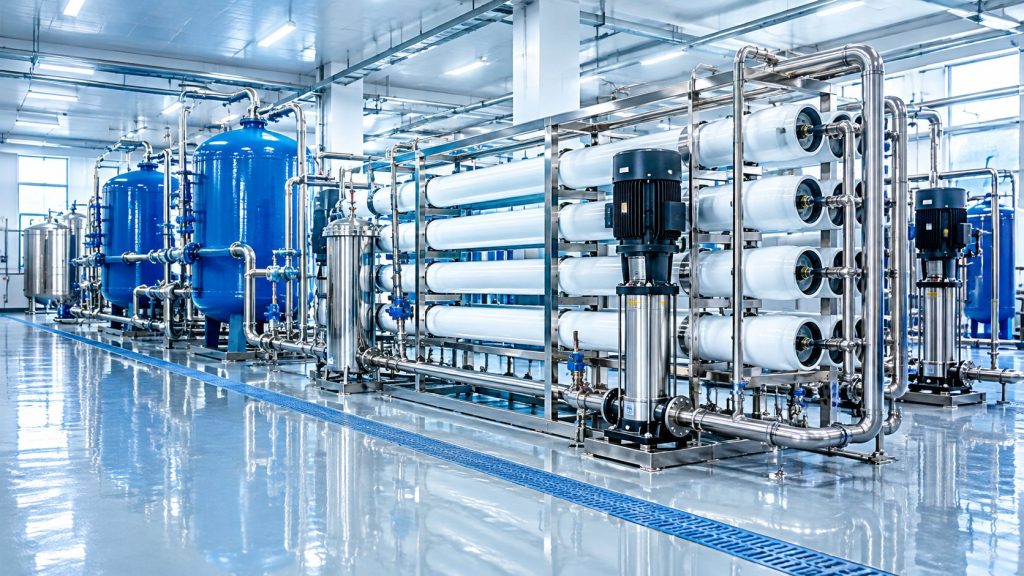 WaterWater Purification Equipment SolutionTreatment and reuse for process water, scalding tanks and plant supply.View solution →
 CleaningFood Industry Cleaning Equipment SolutionsFoam, CIP and washdown systems for food-contact surfaces and drains.View solution →
 PoultryComplete Poultry Slaughter Line SolutionsHanging, scalding, plucking, evisceration and chilling on one continuous line.View solution →