Introduction to Large-Scale Reverse Osmosis Systems
In the realm of industrial water treatment, the demand for high-capacity, reliable purification systems is ever-growing. The 100T/H large-scale reverse osmosis (RO) water treatment system stands as a cornerstone solution for municipal water plants and industrial facilities requiring vast quantities of ultra-pure water. NPW, a leading global manufacturer of integrated industrial equipment, delivers cutting-edge RO technology designed to meet the most stringent water quality standards.
Key Features and Technical Advantages
Our 100T/H RO system is engineered for continuous operation, offering unparalleled efficiency and durability. Key features include:
- High-Flow Capacity: Produces 100 tons of purified water per hour, ideal for large-scale applications.
- Advanced Membrane Technology: Utilizes premium RO membranes for superior salt rejection and consistent performance.
- Robust Construction: Built with food-grade stainless steel (SS304/316) for corrosion resistance and long service life.
- Intelligent Control System: PLC-based automation with touch screen interface for real-time monitoring and easy operation.
- Energy Efficiency: Equipped with high-pressure pumps and energy recovery devices to minimize power consumption.
- Comprehensive Pre-Treatment: Multi-media filters, activated carbon filters, and precision cartridge filters ensure optimal membrane protection.
Applications Across Industries
This large-scale RO system is versatile and finds application in:
- Municipal Water Supply: Providing clean, safe drinking water for communities.
- Food and Beverage Processing: Meeting stringent hygiene standards for product quality.
- Pharmaceutical and Biotechnology: Producing water for injection (WFI) and process water.
- Power Generation: Supplying boiler feedwater and cooling water.
- Electronics Manufacturing: Delivering ultrapure water for semiconductor production.
Quality Assurance and Delivery
At NPW, quality is paramount. Each 100T/H RO system undergoes rigorous testing and inspection before shipment. We ensure proper packaging with shock-absorbing materials and secure fastening to withstand international transport. Our logistics team coordinates delivery to ensure timely arrival and provides comprehensive installation and commissioning support.
Investing in a high-capacity RO system from NPW means partnering with a trusted expert dedicated to your water treatment success.
Why Choose NPW?
With decades of experience in industrial equipment manufacturing, NPW combines innovative engineering with reliable after-sales service. Our 100T/H RO systems are designed for minimal maintenance and maximum uptime, backed by a global network of technical support. Whether you are upgrading an existing plant or building a new facility, NPW delivers tailored solutions to meet your specific water quality and capacity requirements.
Contact NPW today to learn more about how our large-scale reverse osmosis systems can enhance your water treatment operations.
Solutions related to this article
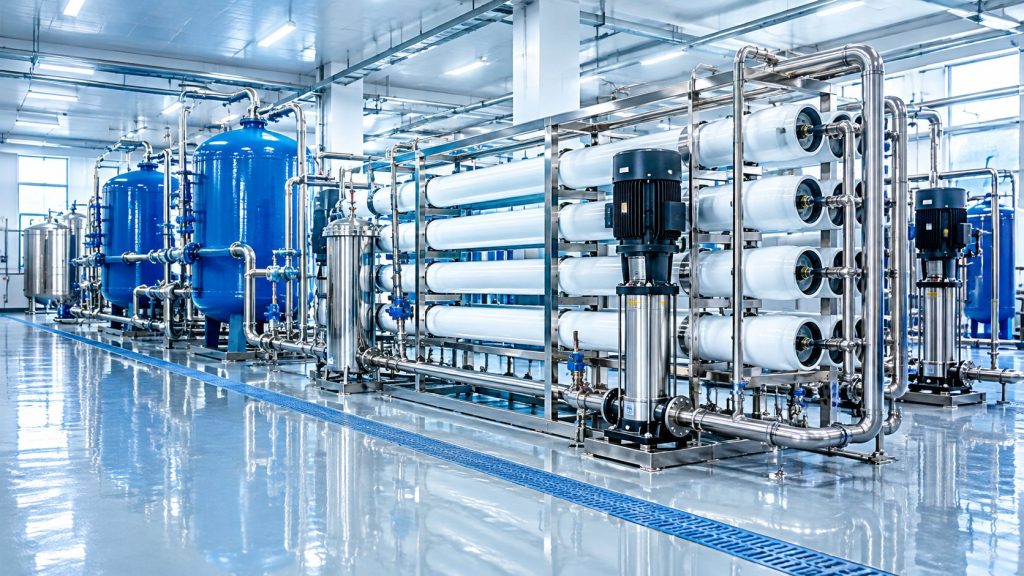 WaterWater Purification Equipment SolutionTreatment and reuse for process water, scalding tanks and plant supply.View solution →
 CleaningFood Industry Cleaning Equipment SolutionsFoam, CIP and washdown systems for food-contact surfaces and drains.View solution →
 PoultryComplete Poultry Slaughter Line SolutionsHanging, scalding, plucking, evisceration and chilling on one continuous line.View solution →