Introduction to the 1.5T/H Fully Stainless Steel Reverse Osmosis System
In the food and beverage industry, water quality is paramount. The 1.5T/H Fully Stainless Steel Reverse Osmosis (RO) Water Treatment System from NPW is engineered to deliver high-purity water for critical processing applications. With a capacity of 1.5 tons per hour, this system ensures a consistent supply of demineralized water, essential for maintaining product quality, safety, and compliance with stringent industry standards.
Key Features and Benefits
- Fully Stainless Steel Construction: The entire system, including the pre-treatment tanks, pumps, and RO membrane housings, is constructed from high-grade stainless steel (SS304 or SS316). This provides exceptional corrosion resistance, ensuring longevity and hygiene in demanding food processing environments.
- High-Efficiency RO Membranes: Equipped with advanced composite membranes, the system achieves a salt rejection rate of over 98%, effectively removing dissolved solids, bacteria, and other impurities.
- Precision Control System: A PLC-based control panel with touch screen interface allows for real-time monitoring of key parameters such as pressure, flow rate, and water quality. Automated flushing and alarm functions ensure optimal performance and reduce manual intervention.
- Compact Skid-Mounted Design: The system is pre-assembled on a compact skid for easy installation and space-saving integration into existing production lines.
- Energy Efficiency: High-pressure pumps and energy-recovery devices (optional) minimize power consumption, reducing operational costs.
Applications in Food Processing
This RO system is ideal for a wide range of food processing applications, including:
- Beverage Production: Providing consistent water quality for soft drinks, juices, and bottled water.
- Ingredient Water: Used in recipes where water composition affects taste and shelf life.
- Boiler Feed Water: Preventing scale buildup in steam generation systems.
- Washing and Rinsing: Ensuring that produce and equipment are rinsed with contaminant-free water.
- Ice Production: Producing clear, pure ice for display and preservation.
Quality Assurance and Compliance
NPW’s RO systems are designed and manufactured to meet international standards for food safety. The use of stainless steel eliminates the risk of plastic leaching and ensures that the water remains free from harmful chemicals. Each system undergoes rigorous testing before shipment, including pressure tests, leak tests, and water quality analysis, to guarantee reliable performance upon arrival.
Conclusion
Investing in the NPW 1.5T/H Fully Stainless Steel RO Water Treatment System means investing in the quality and safety of your food products. With its robust construction, advanced technology, and efficient operation, this system is a valuable addition to any food processing facility. Contact NPW today to learn more about how our water treatment solutions can enhance your production processes.
Solutions related to this article
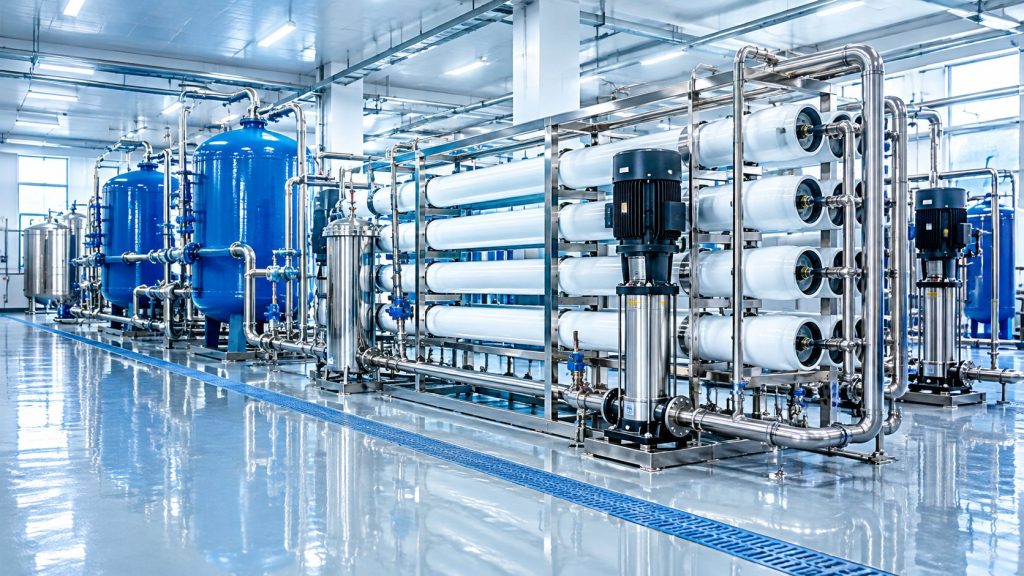 WaterWater Purification Equipment SolutionTreatment and reuse for process water, scalding tanks and plant supply.View solution →
 Steam & HeatingSteam Boiler & Heating System SolutionSteam and hot water for scalding, cleaning, cooking and plant heating.View solution →
 PoultryComplete Poultry Slaughter Line SolutionsHanging, scalding, plucking, evisceration and chilling on one continuous line.View solution →