Introduction to 0.5T/H Reverse Osmosis System
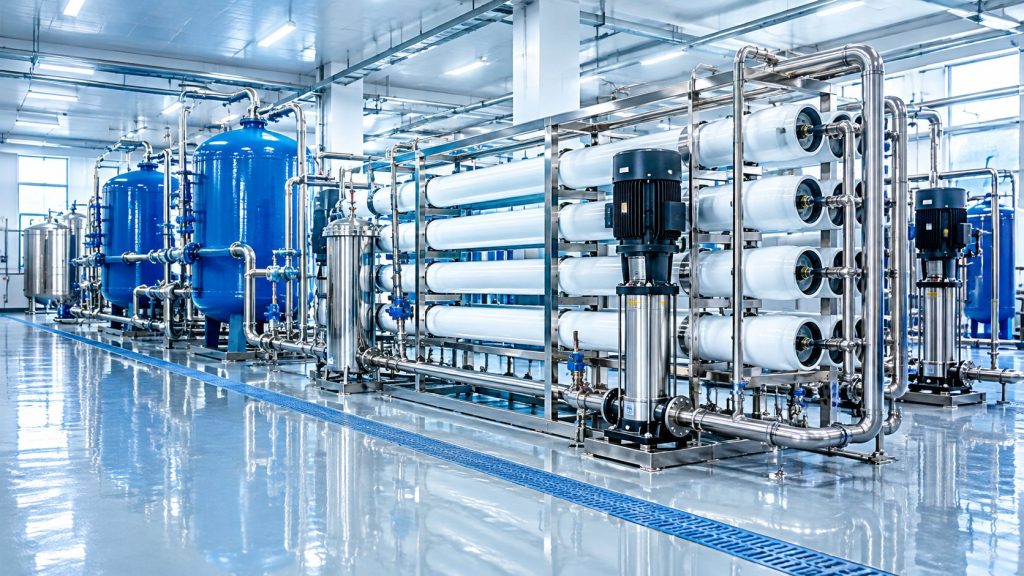
In the food and beverage industry, water quality is critical. The 0.5T/H reverse osmosis (RO) system from NPW is designed to deliver high-purity water for various processing needs. With a capacity of 0.5 tons per hour, this compact system is ideal for small to medium-scale operations, ensuring consistent water quality for production and supporting food industry cleaning equipment throughout the plant.
Key Features and Benefits
Our RO system incorporates advanced membrane technology and robust construction to ensure reliable performance. Key features include:
- High-efficiency membranes: Remove up to 99% of dissolved salts, bacteria, and organic compounds.
- Stainless steel housing: Durable and corrosion-resistant, suitable for hygienic environments.
- Automatic control: PLC-based system for easy operation and monitoring.
- Compact design: Space-saving footprint for easy integration into existing lines.
Benefits include reduced downtime, lower operating costs, and consistent water quality, which is essential for product consistency and safety.
Applications in Food Processing
The 0.5T/H RO system is widely used in food and beverage production, including:
- Ingredient water for beverages, sauces, and soups.
- Water for dough preparation and pasta production.
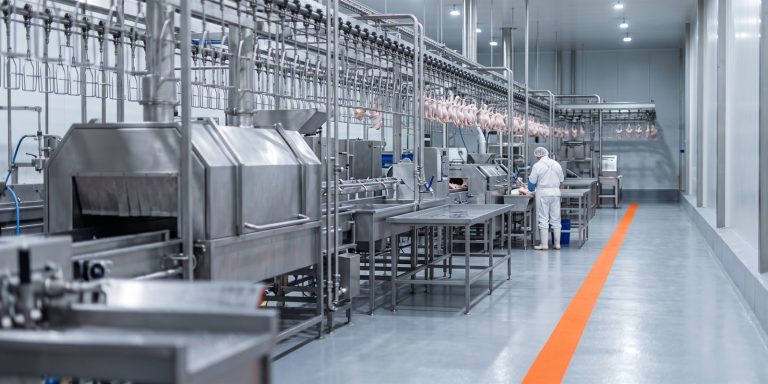
- Rinse water for fresh produce and meat processing, often delivered through a food grade hose.
- Boiler feed water and cooling tower makeup.
By removing impurities, the system helps extend shelf life and maintain flavor profiles. Treated water also protects equipment such as a hot water pressure washer and a commercial steam boiler from scale and corrosion.
Quality Assurance and Delivery
At NPW, we prioritize quality from manufacturing to delivery. Each RO system undergoes rigorous testing before shipment, including pressure tests and water quality checks. We ensure proper packaging to prevent damage during transit, so your system arrives ready for installation.
“Our 0.5T/H RO systems are engineered for reliability and ease of use, helping food producers achieve consistent water quality,” says a NPW engineer.
Conclusion
Investing in a 0.5T/H reverse osmosis system from NPW is a smart choice for food and beverage manufacturers seeking a dependable water treatment solution. With advanced features and robust construction, it ensures pure water for your production needs. Contact NPW today to learn more.
Solutions related to this article
 WaterWater Purification Equipment SolutionTreatment and reuse for process water, scalding tanks and plant supply.View solution →
 Steam & HeatingSteam Boiler & Heating System SolutionSteam and hot water for scalding, cleaning, cooking and plant heating.View solution →
 PoultryComplete Poultry Slaughter Line SolutionsHanging, scalding, plucking, evisceration and chilling on one continuous line.View solution →